The evolution of outdoor protective gear has seen a significant shift toward versatility and maximum coverage. While the industry traditionally focused on standard sizing, there is a growing global demand for specialized equipment, such as an extra long raincoat, to ensure that users remain dry from shoulder to ankle during extreme weather conditions.
In the context of modern textile manufacturing, the integration of high-performance materials like Oxford and Polyester with waterproof coatings has revolutionized how we approach weatherproofing. Whether it is for industrial use, emergency response, or leisure activities, the priority has shifted toward durability and the ability to withstand harsh environmental stressors without compromising the user's mobility.
Understanding the technical specifications of high-coverage gear allows consumers and procurement officers to make informed decisions. By focusing on the intersection of material science and ergonomic design, the extra long raincoat serves as a benchmark for protective apparel that balances comprehensive protection with practical usability in diverse climates.
Global Significance of High-Coverage Gear
Across various continents, the unpredictability of weather patterns has increased the reliance on heavy-duty waterproof apparel. From the monsoon seasons in Southeast Asia to the unpredictable rains of Northern Europe, the need for an extra long raincoat has transitioned from a niche requirement to a mainstream necessity for outdoor laborers and enthusiasts.
Industrial standards, such as those outlined by ISO for personal protective equipment (PPE), emphasize the importance of full-body coverage to prevent hypothermia and maintain operational efficiency. When moisture penetrates clothing, it not only causes discomfort but significantly increases the risk of health complications, making high-coverage waterproof solutions a critical component of workplace safety.
Defining the Modern Extra Long Raincoat
An extra long raincoat is more than just a standard piece of outerwear; it is a specialized garment designed to extend protection well below the knee, often reaching the ankles. Unlike short jackets or standard ponchos, this design ensures that legs and lower-body clothing remain dry, which is essential for those working in muddy environments or facing driving rain.
In terms of modern industrial application, these garments are often crafted from high-density Oxford or Polyester fabrics. The addition of a waterproof coating creates a barrier that prevents water molecules from penetrating the weave, while the extended length minimizes the "splash-back" effect that typically occurs when water hits the ground and bounces onto the wearer's trousers.
This category of protective wear is closely linked to humanitarian needs in disaster-relief zones. In areas where permanent shelter is unavailable, a durable, full-length waterproof layer provides a critical first line of defense against the elements, offering dignity and safety to individuals in precarious living conditions.
Core Components of Waterproof Textiles
The effectiveness of an extra long raincoat depends primarily on the quality of the base textile. Oxford fabric is frequently chosen for its strength and tear resistance, ensuring that the garment can withstand the physical rigors of outdoor activity without ripping.
Waterproof coatings are the secret to the garment's functionality. By applying a specialized chemical or polymer layer to the Polyester or Oxford weave, manufacturers create a hydrophobic surface that causes water to bead and roll off, a feature that is indispensable for any high-quality extra long raincoat.
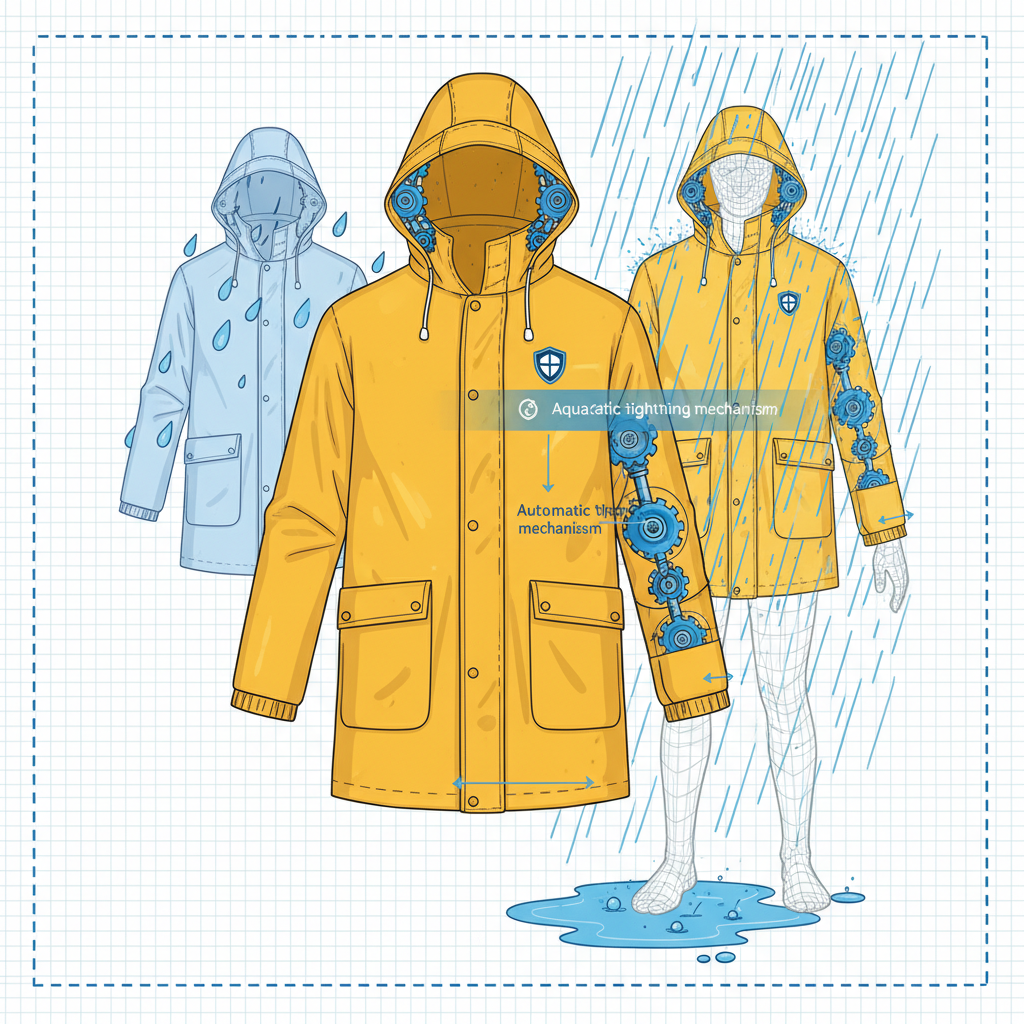
Beyond the fabric, the construction details—such as reinforced seams and secure closures—play a vital role. For a full-length garment, maintaining the integrity of the stitching is crucial to prevent leaks at the stress points, ensuring the wearer stays dry regardless of the storm's intensity.
Performance Metrics in Protective Wear
Evaluating the quality of weather-resistant gear requires a look at specific performance metrics. Durability is measured by the fabric's denier and its resistance to abrasion, while waterproofness is tested by the amount of water pressure the fabric can withstand before leaking. For an extra long raincoat, these metrics are critical because the larger surface area is more exposed to environmental wear.
Scalability in production also plays a role, as OEM designs allow for customization in size and length to fit different body types. This ensures that the "extra long" aspect of the garment is proportionate to the user, preventing tripping hazards while maintaining maximum coverage.
Performance Rating of Various Protective Gear Designs
Real-World Applications and Use Cases
The practical application of an extra long raincoat extends far beyond simple rain protection. In agricultural sectors, workers utilize full-length waterproof gear to protect themselves from pesticide sprays and mud during planting seasons. Similarly, in the logistics industry, delivery personnel in rainy urban centers rely on these garments to keep their uniforms dry throughout long shifts.
In more extreme scenarios, such as post-disaster relief operations, these garments are deployed by NGOs to protect volunteers and victims from damp conditions. The ability to maintain a dry core body temperature is a fundamental aspect of survival and health in remote industrial zones or emergency camps, highlighting the social impact of high-coverage waterproof apparel.
Long-Term Value and Sustainability
Investing in a high-quality extra long raincoat offers significant long-term value through reduced replacement frequency. By using durable materials like coated Oxford fabric, these garments avoid the "fast fashion" cycle of disposable rain gear, thereby reducing plastic waste in landfills.
From an emotional perspective, providing reliable protection fosters a sense of security and dignity. Whether it is a worker feeling valued by their employer through the provision of quality PPE or an outdoor enthusiast feeling confident in their equipment, the reliability of the gear builds a foundation of trust.
Furthermore, the move toward sustainable coatings—reducing the reliance on harmful PFCs (perfluorinated compounds)—shows the industry's commitment to ecological balance. Combining longevity with eco-friendly manufacturing ensures that protective gear serves both the user and the planet.
Future Innovations in Weatherproofing
The future of the extra long raincoat lies in the integration of smart textiles. We are seeing the emergence of breathable, waterproof membranes that allow moisture vapor to escape from the inside while preventing liquid water from entering, solving the common "greenhouse effect" associated with traditional waterproof coatings.
Automation in the manufacturing process is also allowing for more precise ergonomic tailoring. Through 3D body scanning, the "extra long" dimensions can be customized to the millimeter, ensuring that the garment provides maximum coverage without impeding the user's gait or movement.
Additionally, the integration of recycled polyester from ocean plastics is becoming a standard for premium lines. This transformation ensures that the protective gear of tomorrow is not only functional and durable but also part of a circular economy.
Comparative Analysis of Material Performance for Full-Length Protective Gear
|
Material Type
|
Waterproof Rating
|
Durability Score
|
Breathability
|
| Coated Oxford |
High |
9/10 |
Low |
| Coated Polyester |
High |
7/10 |
Medium |
| PVC Vinyl |
Very High |
6/10 |
Very Low |
| Recycled PET |
Medium-High |
8/10 |
Medium |
| Gore-Tex Blend |
Extreme |
8/10 |
High |
| Nylon Ripstop |
Medium |
10/10 |
High |
FAQS
An extra long raincoat provides comprehensive lower-body protection, preventing water from splashing onto trousers and shoes. This is essential for those working in heavy rain or muddy environments, as it keeps the wearer significantly drier and helps prevent hypothermia by reducing moisture absorption in the lower extremities.
Oxford fabric is generally more durable and resistant to tears, making it ideal for industrial or heavy-duty use. Polyester is often lighter and can be more breathable. The choice depends on whether the user prioritizes extreme durability (Oxford) or a lightweight feel (Polyester), though both are excellent when combined with a waterproof coating.
To maintain the coating, avoid using harsh detergents or machine-drying on high heat, which can degrade the polymer layer. Instead, wipe the surface with a damp towel and air dry. If the water stops beading, a specialized waterproof spray can be applied to rejuvenate the hydrophobic surface.
Yes, through OEM services, these garments can be customized with Pantone colors and custom logo printing. This allows companies to maintain brand visibility while providing their staff with high-quality, professional protective gear that meets safety standards.
While they provide more coverage, the added length can act as a sail in high winds. To counter this, look for designs with adjustable drawstrings or side slits that allow for better mobility and wind resistance without sacrificing the protective length of the garment.
Depending on the material, a high-quality coated Oxford raincoat can last several years with proper care. In industrial settings with daily wear and tear, they typically maintain peak performance for 1-3 years before the waterproof coating requires maintenance or the fabric shows significant wear.
Conclusion
The shift toward high-coverage waterproof apparel, exemplified by the extra long raincoat, reflects a broader industrial commitment to durability, user safety, and environmental resilience. By combining advanced textile engineering—such as the use of coated Oxford and Polyester—with an ergonomic focus on full-body protection, these garments solve the critical problem of moisture infiltration in challenging climates.
Looking forward, the integration of sustainable materials and smart textile technology will only enhance the value of these protective solutions. Whether for industrial application, humanitarian aid, or outdoor leisure, investing in comprehensive weatherproofing is a strategic move toward greater efficiency and well-being. For premium, customizable waterproof solutions, visit our website: www.mayraincoat.com
 rainwears@163.com may@may-rain.com
 Mon to Friday: 8.00 am - 7.00 pm